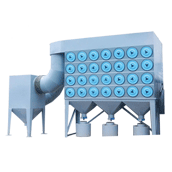


XTD Ceramic Multi-tube Cyclone Dust Collector for Industrial Flue Gas Treatment
Introduction:Industrial boilers, kilns and crushing lines generate large volumes of high-temperature flue gas that carries abrasive and mildly corrosive dust, a duty where ordinary metal cyclones wear out quickly and electrostatic precipitators demand heavy investment. The XTD ceramic multi-tube cyclone dust collector answers this problem with dozens of parallel ceramic cyclone tubes housed in a shared inlet, outlet and ash hopper assembly. Its ceramic inner surface is smooth, wear-resistant and acid-alkali resistant, so it holds efficiency far longer than cast iron separators. Dust removal efficiency reaches 92~95% at a system resistance of only 900~1000 Pa, and the dry process consumes no water and discharges no wastewater. Installed as a pre-dedusting stage ahead of a Dust Collector Filter baghouse, and with a properly selected Air compressor filter protecting the auxiliary air line, it forms a low-cost two-stage dedusting station for metallurgy, mining, building materials, chemical and boiler flue gas projects.
We're here to help:
Easy ways to get the answers you need.
Product parameter:
Product Introduction
The XTD ceramic multi-tube cyclone dust collector is a high-performance dry dust removal unit assembled from dozens of parallel ceramic cyclone elements. It can be configured with ordinary ceramic cyclone tubes or straight-flow cyclone elements, all integrated into a shared housing fitted with a main air inlet, air outlet and ash hopper. As a durable Dust Collector Filter stage for coarse to medium dust, the unit also coordinates with a matched Air compressor filter on the auxiliary air line, protecting the blowback and inspection air supply in the wider dedusting station. Different from traditional cast iron cyclone separators, its core cyclone tubes are made of ceramic material, featuring smoother surface, superior wear resistance and excellent acid and alkali resistance, which supports both dry dust collection and wet dust removal duty. It is designed to capture non-sticky dry dust particles from boiler flue gas, and has become a practical dust control solution for metallurgy, mining, building materials, chemical processing and other heavy industrial sectors. The ash hopper can be fitted with several automatic ash discharge structures to meet continuous production requirements of different plants.
Working Principle

Dust-laden flue gas enters the gas distribution chamber through the main inlet pipe, then flows into the annular gap between the ceramic cyclone body and the guide vane assembly. The guide vanes convert linear airflow into high-speed rotational swirling flow. Most of the rotating gas spirals downward along the inner wall of the ceramic cone. Under the centrifugal force generated by rotation, denser dust particles are thrown toward the inner wall. After contacting the wall they lose kinetic energy and slide down under gravity, finally falling into the ash hopper and being collected as separated ash.
After dust separation, the outer swirling airflow continues downward to the bottom of the cone section. The tapered structure compresses the airflow and reverses its rotation, forming an upward inner spiral of clean gas. This purified gas rises along the central axis of the tube, passes through the exhaust pipe of each ceramic cyclone unit, converges in the exhaust chamber and leaves through the main exhaust port. Depending on site layout, the main exhaust pipe can be arranged on the side of the equipment or on the top for flexible piping.

Main Technical Parameters
| Item | Specification |
|---|---|
| Dust removal efficiency | 92% ~ 95% |
| System resistance | 900 ~ 1000 Pa |
| Inlet flow velocity | 10 ~ 16 m/s |
Model Specification Table
| Model | XTD-1 | XTD-2 | XTD-4 | XTD-6 | XTD-8 | XTD-10 | XTD-15 | XTD-0 | XTD-35 | XTD-75 |
|---|---|---|---|---|---|---|---|---|---|---|
| H4 | 750 | 650 | 500 | 400 | 350 | 400 | 300 | 1000 | 600 | 400 |
| H3 | 1500 | 1500 | 1500 | 1800 | 1800 | 2000 | 2000 | 2800 | 2800 | 2800 |
| H2 | 2450 | 2500 | 2550 | 2850 | 2875 | 3125 | 3200 | 4050 | 4100 | 4350 |
| H1 | 2700 | 2850 | 2900 | 3200 | 3275 | 3525 | 3750 | 4750 | 4750 | 5050 |
| H | 2900 | 3100 | 3150 | 3450 | 3550 | 3800 | 4100 | 5100 | 5150 | 5500 |
| L1 | 420 | 820 | 1220 | 1220 | 1620 | 1620 | 2020 | 2020 | 2440 | 2840 |
| L2 | 820 | 820 | 1220 | 1620 | 1620 | 2020 | 2420 | 3220 | 4440 | 9280 |
| a=b | 200 | 300 | 300 | 300 | 350 | 350 | 500 | 600 | 600 | 600 |
| d | 130 | 130 | 130 | 130 | 130 | 130 | 130 | 130 | 200 | 200 |
| A | 570 | 600 | 1000 | 1300 | 1300 | 1700 | 2100 | 2900 | 4200 | 8700 |
| Flue gas capacity (m³/h) | 3200 | 6400 | 12800 | 19200 | 25600 | 32000 | 48000 | 64000 | 112000 | 240000 |
Core Advantages
Compared with mainstream dust removal solutions, the XTD ceramic multi-tube cyclone dust collector has clear competitive edges for industrial users. First, its overall investment is only about one third of an electrostatic precipitator. Compared with a water film dust collector it adopts dry dedusting technology, consumes no water, produces no secondary pollution and no wastewater discharge, which saves the investment and operating cost of supporting wastewater treatment facilities (except the mist dry dedusting customized version). For plants in water-scarce areas or regions with strict sewage discharge rules, this greatly reduces compliance pressure.
Second, the unit is designed for low maintenance. The ceramic cyclone core is corrosion and wear resistant with a stable structure and almost no vulnerable parts, so daily maintenance workload is extremely low. Owners cut spare parts stock and regular maintenance labor year after year.
Third, it is an energy-saving dust removal system. Like electrostatic precipitators and water film equipment, it only consumes power to overcome flue gas resistance through the induced draft fan; the collector itself needs no extra electrical input, while electrostatic precipitators require continuous high-voltage supply. More than 95% of its raw materials are non-metallic mineral resources available locally, which saves steel resources and lowers the carbon footprint of the whole production chain.
In addition, the modular parallel design brings strong scalability. Users can add or reduce ceramic cyclone tubes according to actual flue gas volume fluctuation, which is convenient for capacity expansion and reconstruction of old workshops. The smooth ceramic inner surface resists dust sticking, avoiding the adhesion and blockage that often occur in cast iron cyclone tubes after long service.
Application Scenarios

The XTD ceramic multi-tube cyclone dust collector is widely used for dry removal of non-sticky particulate dust.
Boiler industry: coal-fired boiler, biomass boiler and waste heat boiler flue gas, working as primary pre-filter before a bag filter or electrostatic system to cut the dust load of downstream fine filtration.
Metallurgy and mining: ore crushing, screening, roasting furnace flue gas and smelting process dust collection.
Building materials: cement raw material grinding, lime kiln, refractory production and ceramic firing flue gas purification.
Chemical industry: drying tower, calcination furnace and chemical powder production exhaust treatment.
Other heavy industries: sand production, asphalt mixing plant and foundry workshop dust control.
It suits working conditions with high flue gas temperature and corrosive gas, where ordinary metal cyclones rust and wear quickly. It can run alone as a primary collector, or be combined with a Dust Collector Filter baghouse to form a two-stage system for stricter emission limits. The matched Air compressor filter protects the air source of auxiliary ash cleaning and inspection lines, keeping the whole dedusting station stable.
Installation, Operation and Maintenance
Installation requirements: install on site according to the working condition, guaranteeing tight sealing without air leakage. External pipes must match the bolt hole pitch of the inlet and outlet flanges; leakage will disorder the internal flow field and directly reduce efficiency.
Air tightness inspection before startup: start the induced draft fan and run a full tightness test. Check welding seams, flange joints and ash discharge valves, and repair leakage points promptly.
Correct startup and shutdown sequence: start the induced draft fan before the furnace is put into operation; when stopping, shut down the fan first and then the furnace. The reverse sequence leads to dust accumulation inside the tubes and rapid flow channel blockage.
Regular ash cleaning: whatever automatic discharge structure is used, regular ash cleaning is mandatory. Excessive ash in the hopper re-entrains dust into the airflow, blocks the cyclone passages and damages performance.
Routine inspection: check ceramic tubes periodically. If a tube is cracked or damaged, replace it in time to avoid airflow short circuit and failure of neighbouring units.
FAQ
Q1: What is the maximum flue gas temperature this XTD ceramic multi-tube cyclone can handle?
A: The ceramic body withstands high temperature. We customize the ceramic formula and sealing structure to actual flue gas temperature. It is commonly used below 400℃, and a high-temperature version is available for hotter duty.
Q2: Can it remove sticky dust and wet dust?
A: It is designed for non-sticky dry dust. Sticky dust adheres to the inner wall and causes quick blockage. For wet dust we can supply the wet dedusting customized version.
Q3: Do I need an Air compressor filter for this dust collector?
A: The cyclone itself does not rely on compressed air for pulse cleaning. If an automatic air blowback ash discharge valve is selected for the hopper, the compressed air line should be fitted with an Air compressor filter to remove oil and water and protect the valve actuator.
Q4: How long is the service life of the ceramic cyclone tubes?
A: Under normal dry, non-corrosive duty the ceramic element works 3–5 years. Life depends on dust hardness, particle concentration and flue gas corrosivity.
Q5: Can it meet emission standards when used alone?
A: Dust removal efficiency is 92~95%. Capture of fine dust below 10μm is limited, so it usually serves as primary pre-dedusting. For ultra-low emission we recommend combining it with a baghouse Dust Collector Filter in a two-stage arrangement.
Related Products
Filter Cartridge Dust Collector lefilter P191526-016-436
P19-1006 Dust Collection Filter Cartridges
P19-1037 lefilter dust collector cartridge filter
Please fill in your procurement needs and contact information